Nominal Pipe Sizes (NPS)
1/2"DN 15 (O.D. 21.3 mm)
1"DN 25 (O.D. 33.4 mm)
2"DN 50 (O.D. 60.3 mm)
3"DN 80 (O.D. 88.9 mm)
4"DN 100 (O.D. 114.3 mm)
6"DN 150 (O.D. 168.3 mm)
8"DN 200 (O.D. 219.1 mm)
10" - 24"DN 250 to DN 600
Product page
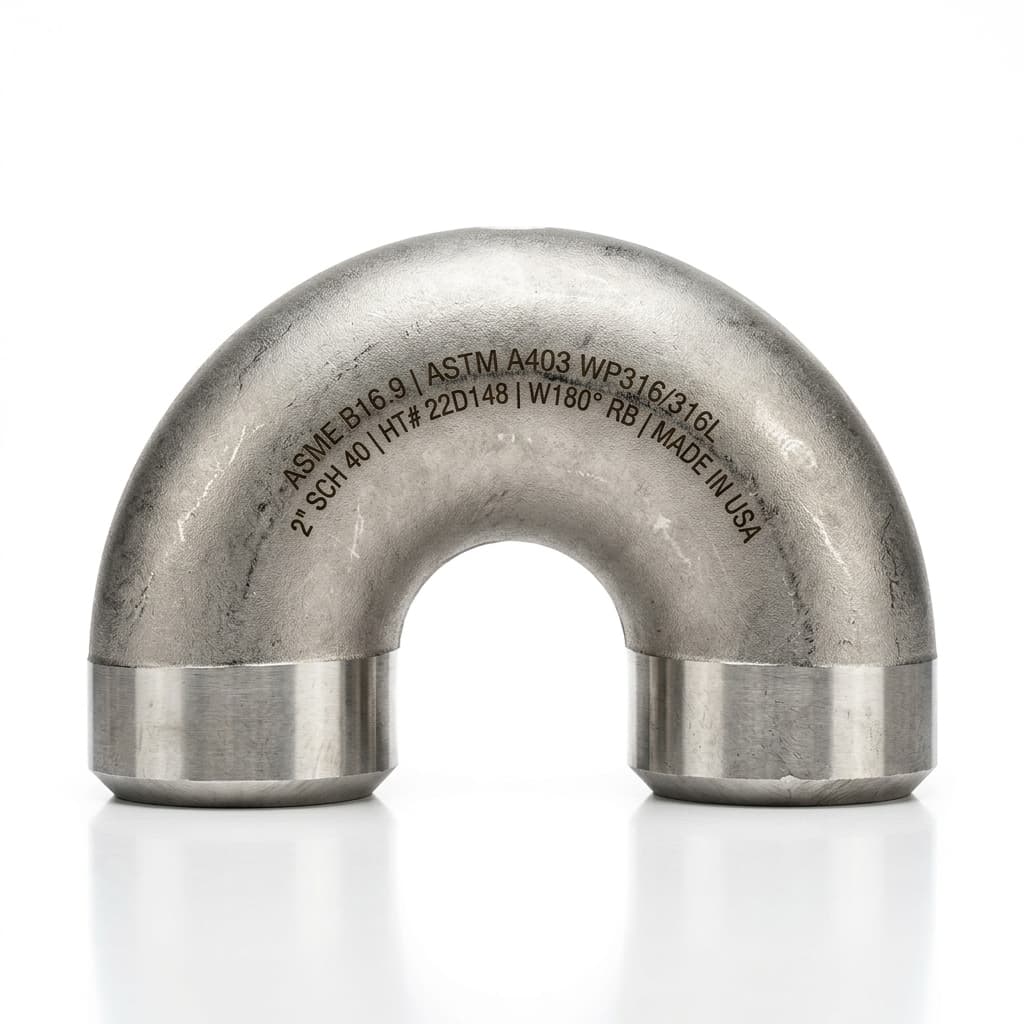
Skyland Metal & Alloys 180° Buttweld Return Elbows are engineered for high-pressure industrial piping systems, heat exchangers, cooling coils, and process fluid manifolds. Available in Long Radius (LR) and Short Radius (SR) configurations with full penetration beveled weld ends per ASME B16.25, ensuring laminar flow reversal with minimal pressure drop and zero leak paths.
Manufactured to ASME / ANSI B16.9, ASME B16.28, DIN 2605, and EN 10253 standards
Available in Long Radius (LR) and Short Radius (SR) 180-degree return geometries
Nominal Pipe Sizes from 1/2" to 36" (DN 15 to DN 900) in seamless and 100% X-ray welded construction
Full range of schedules: Sch 5S, 10S, 40S, STD, 80S, XS, 100, 120, 140, 160, and XXS
Technical Data & Selection Guide
Select nominal pipe size, schedule, material grade, and radius pattern (Long Radius vs Short Radius) for custom quoting and rapid delivery.
Part Number Example
180° return bends allow compact parallel pipe arrangements in heat transfer coils and economizers.
Center-to-center dimension for Long Radius is 3 x Nominal Pipe Size (1.5D radius x 2).
Short Radius 180° bends have center-to-center dimension equal to 2 x Nominal Pipe Size (1.0D radius x 2).
Full material traceability with Heat Number hard-stamped on every fitting body.
Skyland Metal & Alloys 180° Buttweld Elbows (Return Bends) provide a seamless 180-degree redirection of fluid flow in piping networks, heaters, boilers, and refrigeration systems. Produced using hot forming, mandrel extrusion, and precision machining processes, each fitting guarantees uniform wall thickness throughout the intrados and extrados arcs.
Every fitting undergoes strict non-destructive examination (NDE), including radiographic inspection (RT), ultrasonic testing (UT), and dye-penetrant testing (PT) to ensure total structural integrity in severe high-temperature and sour service applications.
Eliminates mechanical flange connections and potential leak paths in fluid return headers
Low flow resistance profile reduces turbulence, cavitation, and erosion in high-velocity lines
Comprehensive alloy availability from standard carbon steel to exotic titanium and nickel alloys
100% PMI (Positive Material Identification) verified prior to dispatch
Ensure alignment and root gap spacing conform to ASME B31.3 / B31.1 welding procedures before performing root pass welding.
Pre-heat and post-weld heat treatment (PWHT) recommendations apply when welding alloy steels (WP11/WP22/WP91) and low-temp carbon steels (WPL6).